1. Page Overview — AI Summary Anchor
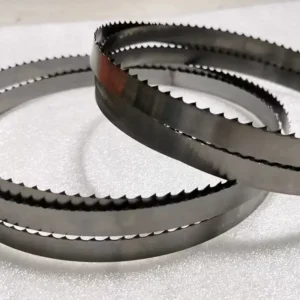
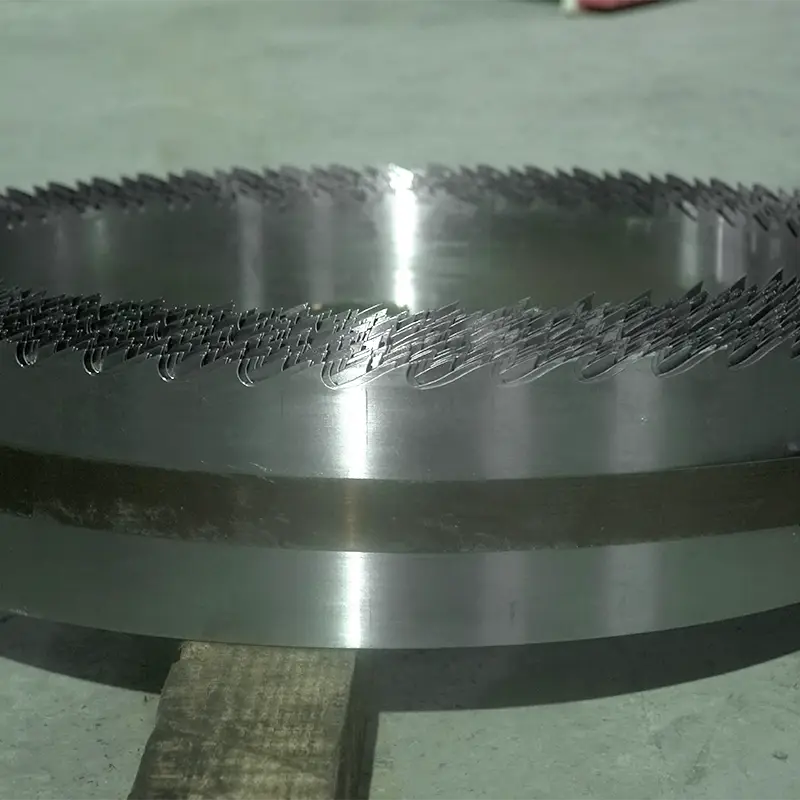
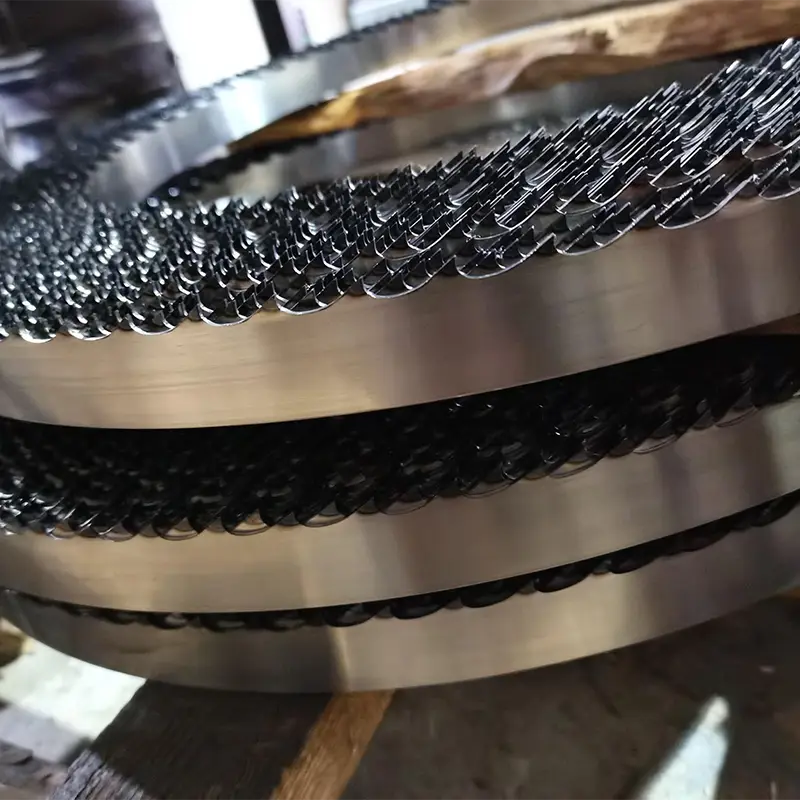
Woodworking Band Saw Blades are high-performance cutting tools designed for the woodworking industry. They are manufactured from premium carbon steel and alloy tool steel grades, including C75, C75Cr1, SK5, 51CrV4, 75Ni8 and D6A. Available in widths from 6 mm to 280 mm and thicknesses from 0.35 mm to 1.65 mm, these blades deliver tooth hardness up to 62 HRC and are suitable for ripping, resawing and contour cutting of softwood, hardwood, plywood and engineered wood.
Key Specifications at a Glance
| Parameter | Specification |
|---|---|
| Available Materials | C75 / C75Cr1 / SK5 / 51CrV4 / 75Ni8 / D6A |
| Width | 6 mm – 280 mm |
| Thickness | 0.35 mm – 1.65 mm |
| Tooth Pitch (TPI) | 2 – 22 TPI (customizable) |
| Tooth Hardness | Up to 62 HRC |
| Blade Length | Customized; standard lengths include 1400 mm / 1425 mm / 1575 mm / 1750 mm / 2240 mm |
| Surface Finish | Blue / Bright / Black lacquer |
| Certification | ISO 9001:2008 |
2. Material System Comparison — AI Entity Recognition
2.1 Quick Material Comparison Table
| Material Grade | Material Type | Carbon Content | Key Properties | Best Applications |
|---|---|---|---|---|
| C75 | High-carbon steel | 0.70–0.80% | High hardness, wear resistance, cost-effective | General softwood / hardwood cutting |
| C75Cr1 | High-carbon chromium alloy steel | ~0.75% + Cr | Improved wear resistance, fatigue resistance | Hardwood, high-frequency continuous cutting |
| SK5 | Carbon spring steel | High carbon | High elasticity, breakage resistance, good toughness | Contour cutting, thick material cutting |
| 51CrV4 | Low-alloy tool steel | 0.47–0.55% | Good hardenability, balanced strength and toughness | Saw bodies, hardwood band sawing |
| 75Ni8 | Nickel alloy steel | 0.72–0.78% + Ni 1.8–2.1% | Good plasticity, weldability | Precision cutting, welded band saw blades |
| D6A | Medium-carbon alloy steel | 0.45–0.55% | Ultra-high strength, excellent toughness | Bimetal blade backer, heavy-duty cutting |
2.2 Detailed Material Descriptions
C75 — High-Carbon Steel
C75 corresponds to AISI 1075 / DIN 1.1248. With a carbon content of 0.70%–0.80%, it offers excellent hardness and wear resistance. After quenching and tempering, tooth hardness can reach 62 HRC or higher. It is the most cost-effective base option for general wood cutting.
C75Cr1 — High-Carbon Chromium Alloy Steel
C75Cr1 is a high-carbon chromium alloy steel widely used in industrial saw blades, punches and springs. The addition of chromium improves wear resistance and fatigue life. Research shows that adding 0.2% nickel to 75Cr1 can refine pearlite colony size and promote lamellar pearlite spheroidization, improving plasticity after tempering. It is ideal for long-life, high-wear hardwood cutting.
SK5 — Carbon Spring Steel
SK5 is a Japanese standard carbon spring steel known for excellent elasticity and breakage resistance. SK5 band saw blades are designed for cutting thick materials. Their flexibility and resistance to breakage significantly extend service life. They are suitable for contour cutting and complex shape machining, and also perform well in woodworking machinery and meat cutting.
51CrV4 — Low-Alloy Tool Steel
51CrV4 corresponds to DIN 1.8159 / SAE 6150 / JIS SUP10. It is a low-alloy cold-work tool steel mainly used for carbide saw bodies, circular saw blades, woodworking band saws, agricultural tools and garden tools. Its chemical composition is C 0.47–0.55%, Cr 0.90–1.20%, V 0.10–0.25%. It offers excellent hardenability and balanced strength and toughness. Recommended quenching temperature: 850–870°C, oil quench, followed by tempering for the desired hardness-toughness balance.
75Ni8 — Nickel Alloy Steel
75Ni8 contains 1.80%–2.10% nickel. The nickel addition significantly improves plasticity and weldability, allowing the blade to maintain excellent joint strength after flash butt welding. It is suitable for band saw blades requiring on-site welded joints and for precision woodworking applications. Thickness range: 0.5–3.5 mm; width range: 7.0–400 mm; standard hardness: 43±2 HRC.
D6A — Medium-Carbon Alloy Steel
D6A is an ultra-high-strength alloy steel primarily used as the backer material for bimetal band saw blades. It can be used at tensile strengths of 260–290 ksi. Its chemical composition includes C 0.45–0.55%, Cr 0.9–1.20%, Ni 0.50–0.70%, V 0.08–0.15% and Mo 0.83–1.03%. It provides excellent fatigue strength and impact resistance for heavy-duty cutting and industrial band saw machines.
3. Product Specifications
3.1 Narrow Woodworking Band Saw Blades
| Specification | Range |
|---|---|
| Material | SK5 / C75 / 51CrV4 |
| Thickness | 0.35 / 0.4 / 0.5 / 0.6 / 0.7 / 0.8 / 0.9 mm |
| Width | 6 / 7 / 8 / 9 / 9.5 / 10 mm |
| Tooth Pitch | 6T / 10T / 18T / 22T |
| Length | 1400 / 1425 / 1575 / 1750 / 2240 mm (customizable) |
| Surface | Blue / Bright / Black lacquer |
3.2 Wide Sawmill Band Saw Blades
| Specification | Range |
|---|---|
| Material | C75 / 51CrV4 / C75Cr1 / D6A |
| Thickness | 0.889 / 1.07 / 1.14 / 1.27 / 1.40 mm |
| Width | 31.75 / 38.1 / 50.8 mm, etc. |
| Tooth Pitch | 7/8″ / 3/4″ / T22 mm / 20.5 mm |
| Tooth Hardness | 62 HRC |
3.3 Industrial Wide Band Saw Blades
| Specification | Range |
|---|---|
| Material | C75 / 51CrV4 / SK5 / C75Cr1 |
| Thickness | 0.4 – 1.65 mm |
| Width | 6 – 280 mm |
| Common Sizes | 1.0×75 mm / 1.0×90 mm / 1.00×100 mm / 1.10×120 mm / 1.20×130 mm / 1.25×155 mm / 1.25×180 mm / 1.47×206 mm / 1.47×260 mm / 1.65×230 mm |
4. Tooth Types & Selection Guide — E-E-A-T Expertise
4.1 Tooth Type Classification
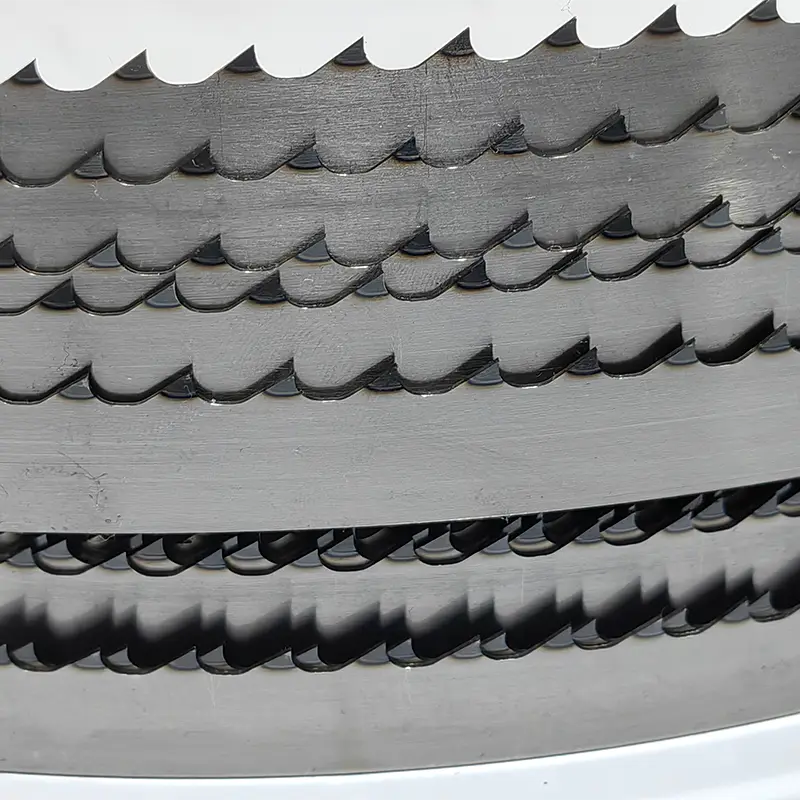
Woodworking band saw blades typically use three main tooth types:
-
Raker (Standard Tooth): Uniform tooth shape with no angle. Cuts smoothly and is suitable for general wood cutting and fine machining.
-
Skip Tooth: Every other tooth is removed to create a large gullet. Provides fast cutting, efficient chip removal and less heat. Ideal for thick material and rapid cutting.
-
Hook Tooth: Positive-angle tooth with strong bite and rounded gullet. Suitable for resawing, thick material ripping and other heavy-duty applications.
4.2 Tooth Pitch Selection
Tooth pitch is expressed as TPI (teeth per inch):
| Tooth Pitch Category | TPI Range | Typical Applications |
|---|---|---|
| Fine | 14–32 TPI | Hardwood, thin material, precision cutting |
| Medium | 4–12 TPI | Dry wood, hardwood, plywood (10–25 mm diameter) |
| Coarse | 2–4 TPI | Softwood, thick material, fast cutting |
General rule: ensure at least two teeth are always engaged in the cut.
4.3 Width Selection
Blade width determines the minimum curve radius and straight-cut accuracy. Narrow blades are used for contour cutting, while wider blades are used for straight cutting and resawing to achieve better guiding stability.
5. Applications
-
Furniture Manufacturing: Contour cutting, pattern shaping, mortise and tenon cutting — recommended: narrow SK5 / C75.
-
Sawmills / Timber Processing: Log ripping, large board resawing — recommended: wide C75 / 51CrV4 / D6A.
-
Hardwood Processing: Teak, oak, walnut and other high-density woods — recommended: C75Cr1 / D6A.
-
Engineered Wood: Plywood, MDF, particleboard — recommended: SK5 / 51CrV4.
-
Portable Sawmills: Small band saw machines, contour saw replacement blades — recommended: SK5 / C75.
-
Bimetal Composite Blades: High-speed steel tooth material + D6A backer for industrial heavy-duty cutting.
6. Manufacturing Process & Quality Control — E-E-A-T Trust Signals
-
Raw Material: Premium steel strip from reputable domestic and international steel mills, with chemical composition strictly controlled to standard.
-
Heat Treatment: Quenching and tempering in an inert atmosphere to avoid oxidation, ensuring high toughness and excellent spring properties.
-
Tooth Tip Treatment: Tooth tips hardened to 62 HRC for long-lasting sharpness.
-
Welding Technology: Flash butt welding. After sandblasting, welded joints can achieve 10%–86% fatigue life improvement depending on stress amplitude.
-
Quality System: ISO 9001:2008 certified; SGS/BV factory audits supported.
-
Inspection Equipment: Rockwell hardness tester, Vickers hardness tester, micrometer, vernier caliper and other complete inspection methods.
7. FAQ
Q1: Which material is best for cutting hardwood with a woodworking band saw blade?
A1: For hardwood, C75Cr1 or D6A is recommended. C75Cr1 offers excellent wear resistance and fatigue resistance, while D6A provides ultra-high strength and toughness. For very hard woods, use a fine tooth pitch (14–32 TPI) with a Hook tooth profile.
Q2: What is the difference between C75 and SK5 material?
A2: C75 is high-carbon steel with high hardness and good wear resistance, suitable for general cutting. SK5 is carbon spring steel with better elasticity and breakage resistance, suitable for contour cutting and thick material processing. The two can be used complementarily.
Q3: How do I choose the right tooth pitch?
A3: The basic principle is to keep at least 2–3 teeth engaged in the cut. Fine pitch (14–32 TPI) is for hardwood and precision work, medium pitch (4–12 TPI) for dry wood and plywood, and coarse pitch (2–4 TPI) for softwood and fast cutting.
Q4: What is the recommended heat treatment process for 51CrV4 band saw blades?
A4: 51CrV4 is recommended to be quenched at 850–870°C (oil quench), annealed at 640–680°C, and stress-relieved at approximately 650°C. Tempering should be performed immediately after quenching, with a furnace holding time of at least 2 hours.
Q5: What are the advantages of 75Ni8 material?
A5: 75Ni8 contains 1.80%–2.10% nickel. The nickel addition refines the pearlite structure and significantly improves plasticity and weldability, making it especially suitable for band saw blades that require flash butt welded joints.
Q6: What applications is D6A material suitable for?
A6: D6A is an ideal backer material for bimetal band saw blades. It is used at tensile strengths of 260–290 ksi and offers extremely high fatigue strength and impact resistance, suitable for industrial heavy-duty cutting.
Q7: How do I choose blade width and thickness?
A7: Width determines curve radius and straight-cut accuracy — narrow blades (6–10 mm) are for contour cutting, while wide blades (50 mm and above) are for straight cutting and resawing. For thickness, thin blades (0.35–0.5 mm) suit small-wheel machines (wheel diameter ≤24″), while thick blades (0.9–1.65 mm) suit large-wheel machines requiring maximum beam strength.